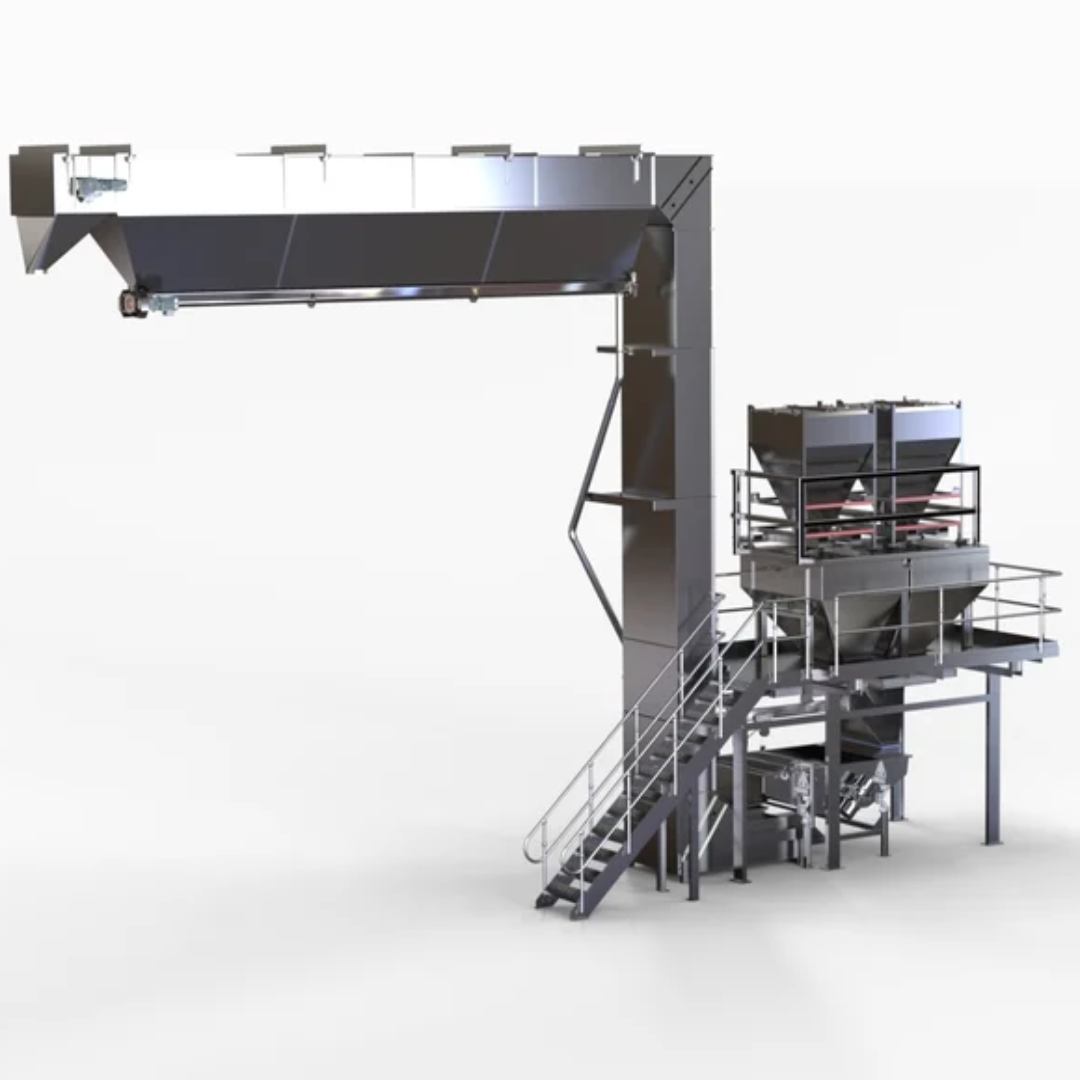
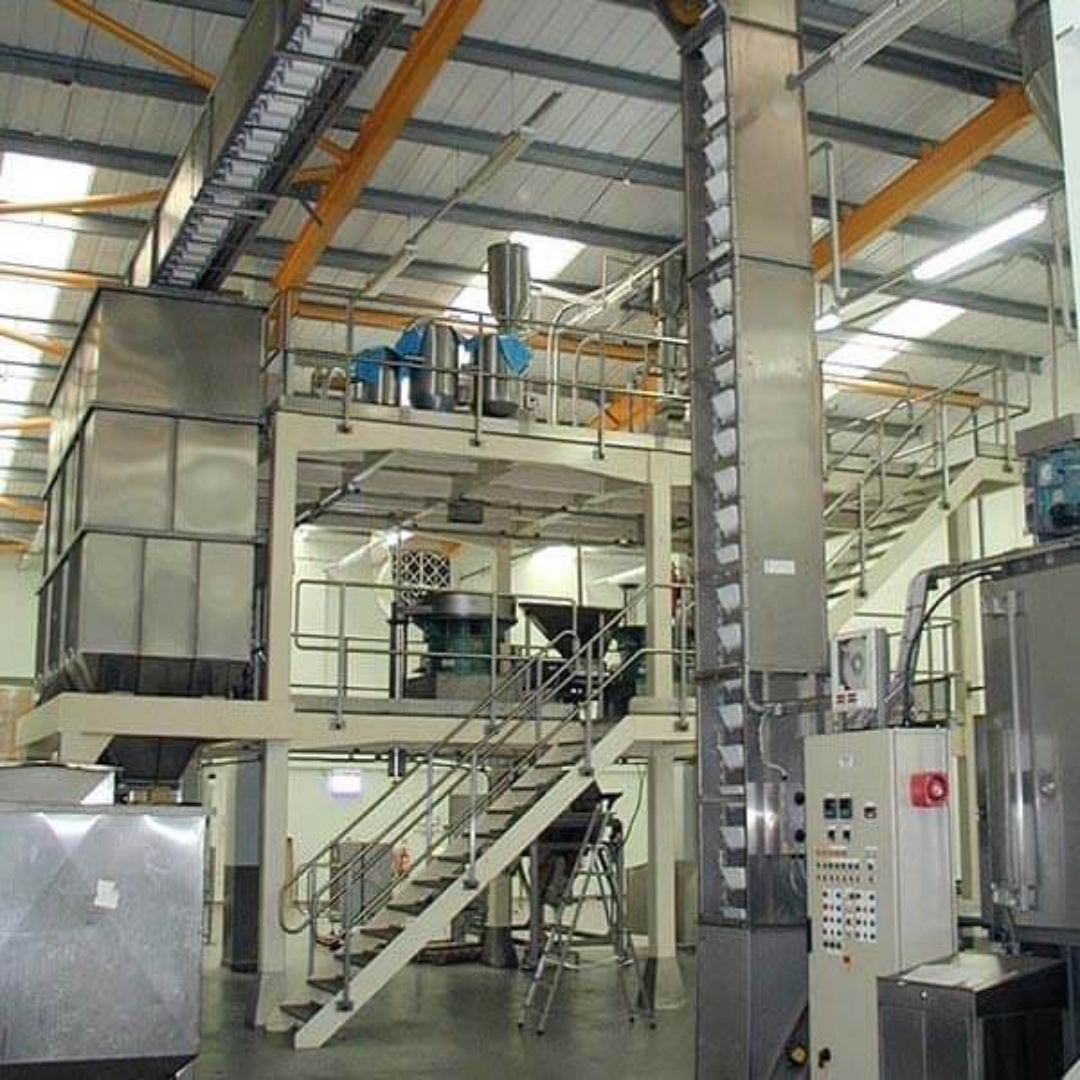
Industrial bucket elevators are vertical conveying systems used to move bulk materials—such as grains, minerals, powders, and aggregates—from a lower level to a higher one in a continuous loop. They consist of a series of buckets attached to a belt or chain, which scoop up or flow in material at the bottom (boot section), lift it vertically, and then discharge it at the head section. These machines are widely used in the agricultural, mining, chemical, cement, food-processing, and construction sectors because they make efficient use of space (vertical lift rather than long horizontal conveyors), can handle large volumes, and protect material integrity thanks to enclosed designs. With options for different discharge styles (e.g. centrifugal, gravity/continuous) and robust construction in materials resistant to wear, corrosion or contamination, bucket elevators are highly adaptable to specific industrial requirements.